
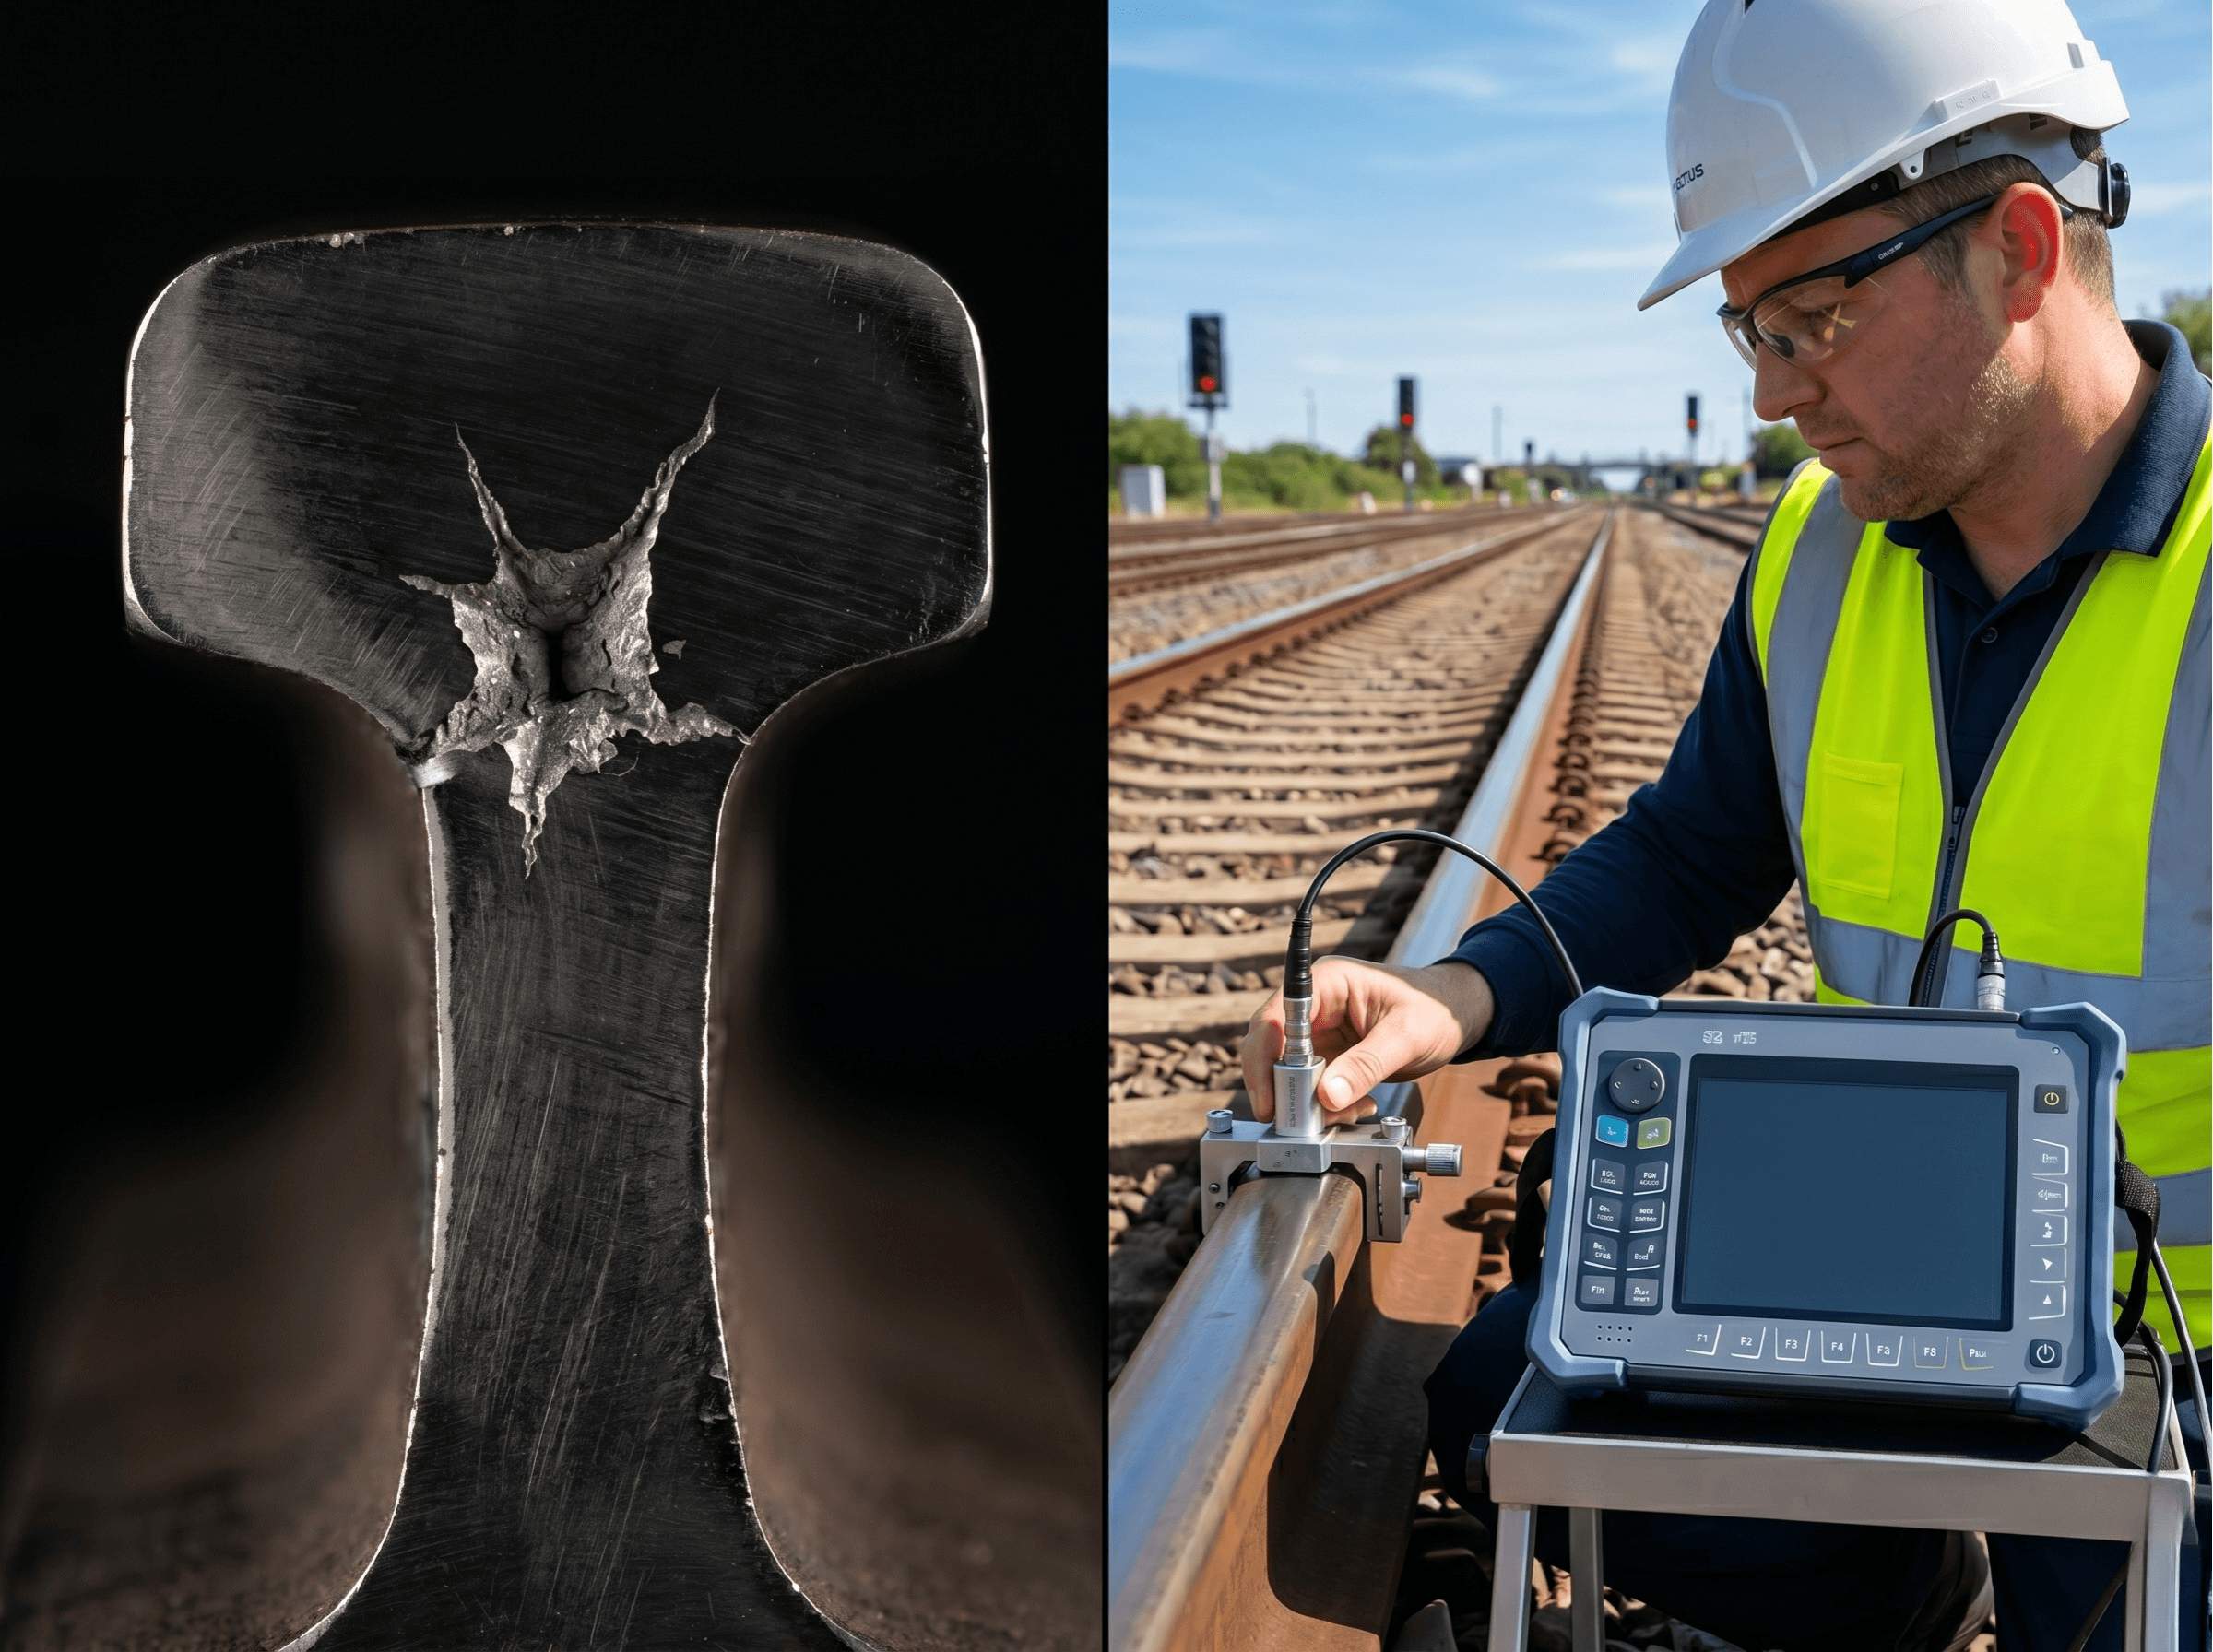
A detail fracture in rail is a progressive crack that starts at or near the surface of the rail head, usually at a shell or head check (49 CFR 213.113(d)(7)). Test systems find it with 70° ultrasonic beams looking forward and backward. At 60% of the head, the rule requires supervision or joint bars plus 50 mph.
This guide is for track supervisors, transit and short-line engineers, and rail flaw test operators. It covers the federal definition, how rolling contact fatigue turns a shell into a detail fracture, how the defect differs from a transverse fissure and a compound fissure, how the 70° channels find it and why shells hide it, the 213.113 remedial actions, and a worked sizing example on 136RE rail.
What is a detail fracture in rail under 49 CFR 213.113?
A detail fracture is a fatigue crack in the rail head that begins at or near the running surface and grows inward, as defined in 49 CFR 213.113(d)(7). The FRA definition, as published on Cornell's Legal Information Institute copy of the eCFR, reads in full:
"Detail fracture means a progressive fracture originating at or near the surface of the rail head. These fractures should not be confused with transverse fissures, compound fissures, or other defects which have internal origins. Detail fractures may arise from shelled spots, head checks, or flaking." — 49 CFR 213.113(d)(7)
Each phrase in the definition does work in the field:
- "Progressive" means the crack grows with traffic. A detail fracture is a fatigue defect, not a single overload break.
- "At or near the surface of the rail head" fixes the origin. This is what separates the detail fracture from defects that start deep inside the steel.
- "Should not be confused with… defects which have internal origins" is FRA telling the reader that the transverse fissure and the compound fissure are different defects, even though all three can end up as a crosswise crack in the head.
- "May arise from shelled spots, head checks, or flaking" names the three surface conditions that start it. All three are forms of rolling contact fatigue. The definition does not name inclusions, which belong to the internal-origin defects.
The definition sits in paragraph (d), the list of 16 defect definitions. The rest of the section decides what happens once a defect is found. Under 213.113(a), a person designated under 49 CFR 213.7 decides whether the track may stay in use, and paragraph (c) holds the remedial action table. The current text is on eCFR, 49 CFR 213.113. It was last amended at 85 FR 63388 (October 7, 2020), a change that touched only the verification sentence in paragraph (b).
How often detail fractures cause derailments
FRA's accident reporting gives the detail fracture its own cause code, T207, "detail fracture from shelling or head check." In FRA train accident data on data.transportation.gov, T207 was the primary cause of 110 of the 384 broken-rail main-track derailments from 2016 to 2025, more than any other rail code (data pulled October 24, 2026). The combined transverse and compound fissure code, T220, accounted for 57 (FRA train accident data). These are derailments, not defects found in testing, and late filings change the counts slightly.
Key takeaway: a detail fracture is defined by where it starts (the surface of the head) and what starts it (shells, head checks or flaking), not by the shape of the final crack.
How does a detail fracture develop from shelling and head checks?
A detail fracture develops when a rolling contact fatigue crack near the gauge corner, usually a shell or a head check, turns downward into the transverse plane of the head and keeps growing under each wheel. The process has three stages, and FRA and TTCI research describe each one.
Stage 1: surface damage forms
Head checks are fine, closely spaced cracks on the gauge corner of the high rail in curves. FRA's research review Rolling Contact Fatigue: A Comprehensive Review (report ORD-11/24, November 2011) says gauge corner cracking occurs "most often on the outer rails of curves and sometimes on tangent rails but infrequently on low rails." As the cracks progress they grow longer and deeper and "may lead to pits and shells" (FRA ORD-11/24, section 1.3.1).
Shells start a little deeper. In a TTCI study of shelled rail on the high-tonnage loop at the Facility for Accelerated Service Testing (FAST), shells "originate as cracks in the subsurface of the high rail gage corner 1/4 to 3/8 inch from the gage corner surface" in 5° and 6° curves. The cracks then grow in a plane parallel to the gauge corner surface until they reach the head surface (TTCI Technology Digest TD-10-004, March 2010). The same digest found that, under 39-ton axle loads, this kind of shell took 20 to 40 MGT from initiation to critical failure. FAST is an accelerated test track, so that figure describes heavy-haul curves, not a typical transit line.
Stage 2: the crack turns down
A shell that stays shallow and breaks out leaves a pit. Part 213 sets no remedial action for shelling alone; in 213.113 the word appears only in the (d)(7) definition. The danger comes when a branch of the crack turns down into the head. Australia's ARTC Rail Defects Handbook (RC 2400, 2006) describes shelling that grows at about 10° to 30° and either spalls out or turns down into a transverse defect (ARTC RC 2400). Some US transit training manuals say the same thing in classification terms: a shell that turns down is classified as a detail fracture from shelling.
FRA's ORD-11/24 adds the steel cleanliness factor. Transverse defects "are initiated by shells in the presence of metallurgical inclusions, most commonly oxide stringers," and their growth "is not a rolling contact phenomenon" but is driven by bending, residual and thermal stress (section 1.3.4). So the shell starts the crack, and the rail's bending stress carries it across the head.
Stage 3: transverse growth to failure
Once the crack is in the transverse plane, it grows with tonnage. The figures in the published record vary widely:
| Source | Reported detail fracture growth | Qualifier |
|---|---|---|
| Earlier studies cited by FRA in the 2014 rule | About 2% of the head's cross-sectional area per MGT | "average development period" for transverse-oriented defects |
| AAR Report R-959 (Davis, Garcia and Snell, September 2002), as cited by FRA | Average growth "exceeded five percent" of head area per MGT | FRA: growth is "inconsistent and unpredictable" |
| NTSB, Superior, Wisconsin derailment (1992) | About 2.5% of head area per MGT | From a 1988 DOT study, applied to that case |
| NTSB, New Brighton, Pennsylvania derailment (2006) | 1.6 to 2.0% of the new head per MGT | An estimate given to the NTSB for heavily worn rail |
Sources: 2014 Improving Rail Integrity final rule, 79 FR 4234 (preamble to 213.113(c) and 213.237); NTSB RAR-08/02; NTSB recommendation letter R-94-1/-2.
The R-959 finding changed the rule. FRA cited it when it lowered the size that triggers the strictest detail fracture actions from 80% to 60% of the head, and when it cut the Class 4 and 5 test interval from 40 to 30 MGT.
Key takeaway: a detail fracture is rolling contact fatigue that turned inward, and once it does, the published growth rates leave little margin between tests.
How is a detail fracture different from a transverse fissure or a compound fissure?
The three defects can all end as a crosswise crack in the rail head, but they start in different places: the detail fracture at the surface, the transverse fissure at an internal nucleus, and the compound fissure from a horizontal split head. The 213.113(d) definitions draw the line:
| Defect | 213.113(d) origin, in the rule's words | Typical location | Remedial action sizing | FRA cause code |
|---|---|---|---|---|
| Detail fracture (d)(7) | "originating at or near the surface of the rail head" from shelled spots, head checks or flaking | Gauge corner of the high rail in curves | % of existing head area: 5–<25%, 25–<60%, 60–<100%, 100% | T207 |
| Transverse fissure (d)(15) | "starting from a crystalline center or nucleus inside the head" | Inside the head, often near the center | Same bands as the detail fracture | T220 |
| Compound fissure (d)(3) | "originating from a horizontal split head that turns up or down" | Inside the head, at the depth of the split | Its own bands: 5–<70%, 70–<100%, 100% | T220 |
The transverse fissure definition adds that its distinguishing features are "the crystalline center or nucleus and the nearly smooth surface of the development which surrounds it." A detail fracture has no internal nucleus: the origin is a surface crack, often under a shell. That difference shows up on the broken face, which is why classification is firmest after a break or once a rail is cut out. For more on the internal-origin defect, see our guide to the transverse fissure in rail.
The compound fissure starts as a horizontal crack, so it begins as a 0° probe target and becomes a 70° target only when it turns. Its development and remedial bands are covered in our article on the compound fissure in rail, and the horizontal defect it grows from is covered in our guide to the horizontal split head.
Why the distinction matters in practice:
- The remedy for a detail fracture and a transverse fissure is the same row. A wrong call between those two changes the record and the cause code, not the speed restriction.
- A compound fissure has different bands. Calling a compound fissure a detail fracture at 65% of head area would give A2 or E and H, where the compound fissure row gives B.
- The cause points to the fix. A detail fracture points to the rail surface, so grinding and friction management are the prevention tools. A transverse fissure points to the steel itself.
Key takeaway: classify by origin. Surface origin means a detail fracture, an internal nucleus means a transverse fissure, and a horizontal split that turned means a compound fissure.
How does ultrasonic testing detect a detail fracture?
Ultrasonic test systems detect a detail fracture with 70° shear-wave beams aimed along the rail in both directions, so that the beam meets the near-transverse crack face at a steep angle and reflects back to the probe. Coverage of the gauge side of the head matters most, because that is where detail fractures start.
Why 70°, and why forward and backward
The refracted angle is measured from the normal to the running surface. A 70° beam travels down and along the rail and strikes a vertical transverse crack 20° off its face, close enough to return a strong echo. A 0° beam runs parallel to that same plane and sees it edge-on. FRA's 2014 rule preamble says UT frequencies "normally" run from 2.25 to 5.0 MHz in flaw detection operations (79 FR 4234, p. 4237).
Real detail fractures are seldom perfectly vertical. A crack that turns down from a shell leans, and a leaning face favors a beam from one side. That is why test systems pair a forward-looking and a backward-looking 70° channel: a crack tilted away from one beam faces the other. The pairing also helps confirm a call, since a true reflector gives echoes from both directions at matching positions.
| Channel | What it does for a detail fracture | Limit |
|---|---|---|
| 70° forward | Main detection beam for transverse cracks in the head | Weak response from a crack leaning away from it |
| 70° backward | Sees the opposite face; confirms the forward call | Same masking by shells as the forward beam |
| 70° gauge-side or skewed channels (on some systems) | Puts beam energy into the gauge corner, where detail fractures start | Channel arrangements vary by system and aren't standardized in US rules |
| 0° | Shows horizontal shell components and loss of bottom | Doesn't see the transverse face; loss of bottom alone may be lost coupling |
| 37–45° | Web and bolt-hole region | Not a head-defect channel |
This is a typical arrangement. No public source names a standard North American rail UT channel set, and 49 CFR 213.237 names no method at all; it requires internal rail inspection with equipment that can find defects between joint bars (49 CFR 213.237). For the beam-angle physics in more depth, see how ultrasonic testing works for railways.
Gauge-side coverage
A 70° beam from a probe centered on the head looks down a band in the middle of the head. A detail fracture that starts at the gauge corner can sit at the edge of that band, or outside it. Two published sources show the issue from different sides:
- TTCI TD-18-027 (Cummings, November 2018) drilled holes across the head of five rails with poor surface condition and hand-scanned them with a 70° probe. Relative to the same hole in a control rail, the average response was 68% on the gauge side, 52% at the center and 80% on the field side. On the detector car, "the field side indications were typically stronger than the center or gage side indications" (TD-18-027). The gauge side, where RCF lives, did not get the strongest response.
- India's RDSO Manual for Ultrasonic Testing of Rails and Welds (Revised 2022) describes a dedicated set-up for "defects originating from Gauge Face and Non-gauge Face Corner": three 70° probes "covering approx. the full width of the rail head," run forward and backward, with the statement that "a defect located at 5mm from the corner is detectable" (RDSO USFD Manual). It isn't a US requirement, but it shows how one national railway designs coverage for corner-origin cracks.
The practical point for a buyer: ask how the proposed system covers the gauge corner on the high rail of curves, and whether that coverage is shown on a reference rail with a gauge-corner reflector.
Confirming and sizing by hand
A test-car call is a suspect until a qualified operator verifies it. The operator returns to the mark with a hand probe, confirms the 70° echo from both directions, and sizes the crack. Depth comes from the sound path: depth = sound path × cos 70°. Extent across the head comes from moving the probe across the head and noting where the echo is lost. The size is then expressed as a percentage of the existing head area, which is what the 213.113 table uses. The worked example below runs through the numbers.
Key takeaway: the 70° pair finds the transverse face, and gauge-side coverage decides whether the beam reaches the corner where detail fractures begin.
Why do shells hide detail fractures from ultrasonic testing?
Shells hide detail fractures because the shell is a crack parallel to the surface that sits between the probe and the defect, reflecting or scattering the beam before it reaches the transverse crack. Since detail fractures start under shells, masking is mainly a detail fracture problem, not a transverse fissure problem.
The benchmark data most often cited for masking comes from TTCI's 1998 tests of six hi-rail systems on the Rail Defect Test Facility near Pueblo, Colorado:
"Results of the six evaluations identify a hit (detected rail flaw) percentage for TDs under shells at approximately 62 percent and the hit percentage for those not under shells at 77 percent." — TTCI TD-99-006, Benchmarking Results of North American Rail-Flaw Detection Technologies (Garcia and Reiff, February 1999)
Read that figure with its qualifiers. It is for transverse defects under shells, seven of them, against 33 with no surface anomaly. Six runs over the same flaws give 26 hits in 42 looks under shells (61.9%, a 95% Wilson interval of about 47–75%) against 152 in 198 without (76.8%, about 70–82%). The intervals overlap, and repeat looks at the same flaw aren't independent. The data is from 1999, and it says nothing about head checks alone.
Other sources agree on the mechanism:
- FRA ORD-11/24 (2011): "the presence of larger and more critical internal defects can be shadowed by smaller surface cracks during inspection" (section 3.1).
- TTCI TD-08-041 (October 2008): "the poor rail surface conditions can diffuse the ultrasonic signal that rail flaw detection vehicles use to find rail defects."
- TTCI TD-16-050 (Witte and Poudel, November 2016): "One of the most difficult defect types for conventional UT inspection to detect is the transverse defect (TD) under shelling. The shelling on the surface of the rail interrupts the acoustic coupling." (TD-16-050)
- NTSB, Superior, Wisconsin (June 30, 1992): the rail failed from detail fractures that started in shelling at the upper gauge corner. The rail had been tested by a UT car about six weeks earlier. The NTSB found that overlapping shelling cracks "prevented the penetration of the ultrasonic sound waves through the head of the rail" (NTSB R-94-1/-2).
Masking has a regulatory consequence. Under 49 CFR 213.237(g), rail over which the qualified operator determines that a valid search could not be made doesn't count as tested. Making that call is part of the operator's authorized duties under 49 CFR 213.238(b)(4). The owner then has three options under 213.237(h): retest, run at no more than 25 mph, or replace the rail. Grinding the shells off before a retest is the usual route back to a valid search; see head checks in rail and rail shelling and spalling for the surface side.
Key takeaway: the shell that starts a detail fracture is also what hides it, so a test over heavy shelling should be recorded as a no-test, not a clean result.
What remedial action does 213.113 require for a detail fracture?
Under 213.113(c), a detail fracture takes remedial action C, D, A2 or E and H, or A or E and H, depending on the percentage of existing rail head cross-sectional area it weakens. The detail fracture shares its bands with the transverse fissure, the engine burn fracture and the defective weld:
| Percentage of existing rail head cross-sectional area weakened by defect | Remedial action (note) |
|---|---|
| 5% to less than 25% | C |
| 25% to less than 60% | D |
| 60% to less than 100% | A2, or E and H |
| 100% | A, or E and H |
Source: 49 CFR 213.113(c), as published in the 2014 final rule, 79 FR 4256. The table is an image on eCFR and Cornell LII, so read it in the Federal Register or the annual CFR PDF. The table hasn't changed since 2014.
What the notes require, from the 2014 rule text:
| Note | Requirement |
|---|---|
| A | "Assign a person designated under § 213.7 to visually supervise each operation over the defective rail." It sets no speed and is not a stop order. |
| A2 | After a visual inspection, the designated person may allow operation without continuous supervision at a maximum of 10 mph for up to 24 hours before another visual inspection or replacement or repair |
| C | Joint bars bolted only through the outermost holes within 10 days. On Class 3–5 track, 30 mph until the bars are on, then 50 mph (or the class maximum, if lower). If the defect was found by a 213.237 internal test, 50 mph is allowed for up to 4 days first. If bars aren't applied within 10 days, 10 mph |
| D | Joint bars bolted only through the outermost holes within 7 days; 30 mph or less, as authorized by a designated person with at least 1 year of supervisory experience, until they are on. If bars aren't applied within 7 days, 10 mph |
| E | Joint bars bolted as required by 213.121(d) and (e) |
| H | 50 mph, or the class maximum if lower |
Points that are often missed:
- "Existing" head area. In 2014 FRA changed the column heading to the "percentage of existing rail head cross-sectional area weakened by defect," so that an operator can't "size transverse defects without accounting for the amount of rail head loss" (79 FR 4243). On worn rail the same crack is a bigger percentage.
- Verification clock. Under 213.113(b), the owner verifies an indication within four hours, or immediately if it points to a defect needing A, A2 or B. The clock runs from when the owner learns of the indication.
- Who decides. The 213.7 designated person decides whether track stays in use (213.113(a)). A rail flaw operator qualified under 213.238 holds a different qualification and isn't that person unless also designated.
For the whole table and every note, see our guide to FRA defect codes.
Key takeaway: size against the existing head, then read the action from the row; 60% is the line where A2 or E and H begins.
Worked example: sizing a gauge-corner detail fracture on 136RE rail
This example sizes a detail fracture from hand-verification readings and shows how head wear moves it from action C to action D. The numbers are illustrative.
Scenario. A scheduled 213.237 test on a Class 4 freight main line carrying 40 MGT a year flags a 70° indication on the high rail of a curve, under visible shelling at the gauge corner. The rail is 136RE. The operator verifies by hand from both directions.
Inputs
| Input | Value | Basis |
|---|---|---|
| New 136RE head width | 2.9375 in. | Mill section data |
| New 136RE head depth | 1.9375 in. (1-15/16 in.) | Mill section data (confirm against the owner's drawing) |
| Shear velocity in rail steel | 0.1280 in./µs (3,250 m/s) | Typical value |
| Deepest 70° echo, sound path | 3.158 in. | Hand probe reading |
| Lateral extent from the gauge face | 1.50 in. | Echo lost when the probe moves past this point |
| Vertical head wear | 0 in. (case 1) and 1/4 in. (case 2) | Measured with a wear gauge |
Step 1: depth of the crack tip
Depth = sound path × cos 70° = 3.158 × 0.3420 = 1.08 in. below the running surface. The surface distance from probe index to the reflector is 3.158 × sin 70° = 2.967 in., and the round-trip time is 2 × 3.158 ÷ 0.1280 = 49.34 µs. On a new head that tip sits at 56% of the head depth (1.08 ÷ 1.9375).
Step 2: crack area
Model the crack as a quarter-ellipse anchored at the gauge corner, with semi-axes of 1.08 in. (down) and 1.50 in. (across):
Area = (π ÷ 4) × 1.08 × 1.50 = 1.272 in²
The quarter-ellipse is a simplification. A real detail fracture under a shell has an irregular outline, and owners usually size from their own charts for each rail section.
Step 3: percentage of the head, new and worn
The head's cross-sectional area isn't in the public mill tables, so this example uses the bounding rectangle, width × depth. The rectangle overstates the true head area because of the corner radii and the fillet under the head, so every percentage below is a lower bound.
| Case | Head area used | Crack area | % of head weakened | 213.113 row |
|---|---|---|---|---|
| 1. New head | 2.9375 × 1.9375 = 5.691 in² | 1.272 in² | 22.4% | 5–<25%: C |
| 2. 1/4 in. vertical wear | 2.9375 × 1.6875 = 4.957 in² | 1.272 in² | 25.7% | 25–<60%: D |
Two lessons come out of the table. First, wear alone moves the same crack across the 25% line, which is exactly why the 2014 rule ties sizing to the existing head. Second, case 1 is close to the line even on new rail. If the true head area is below about 5.09 in² (89% of the rectangle), the new-head case is also over 25%. Near a band boundary, size with the owner's head-area chart, and treat the more restrictive row as the working answer until the size is confirmed.
Step 4: the remedial action
For case 2, action D applies. The verification falls under the four-hour clock in 213.113(b), since D isn't an A, A2 or B action. If the rail isn't replaced, joint bars go on within 7 days, bolted only through the outermost holes. Speed stays at 30 mph or less until then; if the bars aren't on within 7 days, the limit drops to 10 mph.
Had the new-head result stood (case 1, action C), the rule would have allowed 50 mph for up to 4 days because the defect came from a 213.237 test, then 30 mph until bars are applied within 10 days.
Step 5: how much margin the growth rates leave
At the R-959 average of 5% of head area per MGT, the crack would grow from 25.7% to 60% in (60 − 25.7) ÷ 5 = 6.9 MGT. On a line carrying 40 MGT a year, that is about 63 days. At 2.5% per MGT it is 13.7 MGT, about 125 days. FRA called the growth "inconsistent and unpredictable," so treat these as a range, not a forecast. Either way, the 7-day deadline for bars is short compared with the time to the next band, and the 30 MGT test interval is long.
Step 6: the record
The 213.241 record must give the defect's location, type and size, the initial remedial action and its date, and any track not validly tested (49 CFR 213.241). Record the wear measurement with the size, so a later reader can see which head area the percentage used.
Key takeaway: the same crack can be C on new rail and D on worn rail; measure the wear and size against the existing head.
What are the limits of ultrasonic testing for detail fractures?
Ultrasonic testing is the primary method for finding detail fractures, but it can't see past heavy shelling, it sizes by estimate, and it can only show what was in the test. The main limits:
- Masking by shells. Covered above: TD-99-006's 62% under shells (n = 7) against 77% without. A geometry check on 136RE shows why shell length matters. For a crack tip 0.75 in. deep, a 70° beam crosses a shell lying 0.40 in. deep (0.75 − 0.40) × tan 70° = 0.96 in. before it reaches the crack. A shell longer than about 1.9 in. centered on the crack therefore sits in the path of both the forward and the backward beam.
- Small cracks under RCF. A crack that is still shallow and sitting under head checks may give no echo distinct from the surface noise. TTCI found that 90% of 880 RCF cracks and spalls examined by microscopy were 0.040 in. deep or less, and that 3 to 5 grinder passes "would likely have improved UT confidence" (TD-18-027).
- Gauge corner coverage. A centered 70° beam may not reach a crack right at the corner. Coverage depends on the system's channel layout.
- Sizing is an estimate. The percentage of head area is built from a few readings and a shape assumption. The worked example shows how wear and the head-area figure move the answer.
- Surface methods don't replace UT. Visual inspection, eddy current and magnetic particle methods can show the shells and head checks, but not the transverse crack's size inside the head. The TSB of Canada, investigating a 1999 break from shelly rail, stated that "Visual track inspection cannot identify developing fractures from shelly damage" (TSB report R99M0046).
- Coverage of the rail, not just the line. A rail installed after the last test, such as a plug, wasn't searched, whatever the test record says about the line.
For a broader comparison of methods, see our guides to detection of rail defects using NDT methods and detecting rail defects.
How EMA Industries applies this
EMA Industries performs ultrasonic rail flaw testing for transit agencies, short lines and industrial track owners, based in Southern California and mobilizing nationwide. On curves with shelling or head checks, ask any test provider to state how the 70° channels cover the gauge corner and to record every stretch where shelling prevented a valid search. Each detail fracture should be reported with its size, the head wear used for that size, and the matching 213.113 row. To scope a test program, see our ultrasonic rail testing services or contact us.
Related reading: Horizontal split head · Transverse fissure in rail · Compound fissure in rail · Rolling contact fatigue in rail · 49 CFR 213.237 rail flaw detection requirements
Frequently asked questions
What causes a detail fracture in rail?
Rolling contact fatigue at the rail surface. 49 CFR 213.113(d)(7) says detail fractures may arise from shelled spots, head checks or flaking. A crack from one of these turns down into the head and grows under the rail's bending stress, most often at the gauge corner of the high rail in curves.
Is a detail fracture the same as a transverse fissure?
They are different defects with the same remedial action bands. A detail fracture starts at or near the surface of the head; a transverse fissure starts from a crystalline nucleus inside the head. FRA's rule says detail fractures "should not be confused with" defects of internal origin, and FRA accident reporting codes them separately (T207 and T220).
Which ultrasonic probe finds a detail fracture?
The 70° shear-wave probe, run looking forward and backward along the rail. It strikes the near-transverse crack face about 20° off normal and returns an echo. The 0° probe doesn't see the transverse face, though it can show a horizontal shell above the crack.
Can shelled rail hide a detail fracture from a test car?
It can. In TTCI's 1998 benchmark, transverse defects under shells were found about 62% of the time against 77% for those with no surface anomaly, from small samples. When shelling prevents a valid search, 49 CFR 213.237(g) says that rail doesn't count as tested, and the owner must retest, limit speed to 25 mph or replace it.
What happens when a detail fracture reaches 60% of the rail head?
The rail takes remedial action A2, or E and H. A2 lets a 213.7 designated person, after a visual inspection, allow 10 mph for up to 24 hours. E and H means joint bars bolted per 213.121(d) and (e) and a 50 mph limit. At 100% the choice is A (visual supervision of each move) or E and H.
Sources
- 49 CFR 213.113, Defective rails, eCFR; definitions read verbatim on Cornell LII, October 2026
- 49 CFR 213.237, Inspection of rail, eCFR
- 49 CFR 213.238, Qualified operator, eCFR
- 49 CFR 213.241, Inspection records, eCFR
- Track Safety Standards; Improving Rail Integrity, 79 FR 4234 (January 24, 2014), Federal Register (preamble pp. 4243–4248; remedial action table and notes p. 4256)
- FRA ORD-11/24, Rolling Contact Fatigue: A Comprehensive Review (November 2011), ROSA P
- TTCI TD-99-006, Benchmarking Results of North American Rail-Flaw Detection Technologies (February 1999)
- TTCI TD-10-004, rail shell defects at FAST (March 2010)
- TTCI TD-08-041 (October 2008)
- TTCI TD-16-050, Characterizing Rail Flaws Using Phased Array Ultrasound (November 2016)
- TTCI TD-18-027 (November 2018)
- NTSB recommendation letter R-94-1/-2 (Superior, Wisconsin, April 1, 1994)
- NTSB RAR-08/02 (New Brighton, Pennsylvania)
- TSB Canada rail investigation report R99M0046
- ARTC RC 2400, Rail Defects Handbook (2006)
- RDSO, Manual for Ultrasonic Testing of Rails and Welds (Revised 2022), Indian Railways
- FRA train accident data (byy5-w977), data.transportation.gov, queried October 24, 2026