In the thickness gauge vs flaw detector choice, the job decides. Federal rule 49 CFR 213.237 requires internal rail inspections that find defects such as transverse fissures, so scheduled rail testing needs flaw detection equipment and a qualified operator. A thickness gauge measures remaining metal, which is the right tool for web and base corrosion, not for cracks.
Both instruments time ultrasonic echoes in steel. A thickness gauge reports one number, the distance to the back wall. A flaw detector shows the full A-scan, so a trained operator can tell an echo from a crack or weld defect apart from geometry.
This guide maps railway jobs to the right tool, including rail head wear, which needs neither. For how thickness readings are taken and calibrated, see ultrasonic thickness measurement methods.
What is the difference between a thickness gauge and a flaw detector?
A thickness gauge is a measuring instrument that reports how much metal remains between two surfaces; a flaw detector is a search instrument that shows every echo in the sound path so an operator can find and size discontinuities. The physics is shared, but the instruments are tuned for different questions.
Evident, a maker of both instrument types, puts the split simply: a thickness gauge "can accurately measure the thickness of a material", while a flaw detector is "designed to locate and size discontinuities such as cracks, voids, porosity, and disbonds" (Evident, December 2020; vendor source).
| Feature | Ultrasonic thickness gauge | Ultrasonic flaw detector |
|---|---|---|
| What it reports | A thickness number (T = V × t / 2) | An A-scan: echo amplitude against time, read by the operator |
| Typical probes | Dual-element corrosion probes, single-element contact or delay-line probes | Straight-beam (0°) and angle-beam probes (for rail, typically 37–45° and 70°), plus duals |
| Built-in corrections | V-path correction for duals, automatic zero, echo-to-echo through coatings (model-dependent) | DAC, TVG and DGS sizing tools, gates and alarms |
| Main questions answered | How thin is it? How fast is it thinning? | Is there a crack or void? Where is it, and how big does it respond? |
| Governing practices | ASTM E797 for contact pulse-echo thickness | The rule or code for the part: 213.237 for rail, AWS D1.1 for structural welds, owner specifications for rail welds |
| What it misses | Cracks and planar flaws that don't change the back-wall reading | Gradual uniform thinning, unless the operator measures it on purpose |
ASTM E797 describes contact thickness measurement "from one side of the object, without requiring access to the rear surface", and lists corrosion and erosion thinning as a main use (ASTM E797/E797M-21). It is limited to parts no hotter than 93 °C (200 °F) and is "primarily for flat components with parallel surfaces". That last condition matters on rail, where the head, web and base are curved and tapered.
Key takeaway: a gauge answers "how much metal is left"; a flaw detector answers "is there something in the metal that shouldn't be there".
Does FRA 213.237 require a flaw detector or a thickness gauge?
49 CFR 213.237 requires internal rail inspections for defects, so it calls for flaw detection equipment; it contains no thickness or corrosion requirement. Thickness checks don't count toward a 213.237 search at all.
The rule's opening sentence reads:
"In addition to the inspections required by § 213.233, each track owner shall conduct internal rail inspections sufficient to maintain service failure rates per rail inspection segment…" — 49 CFR 213.237(a) on eCFR
Paragraph (f) adds that "Inspection equipment shall be capable of detecting defects between joint bars, in the area enclosed by joint bars." A thickness gauge can't do that, and it can't produce the continuous search the rule describes. Under 213.237(j), a valid search is "a continuous inspection for internal rail defects where the equipment performs as intended and equipment responses are interpreted by a qualified operator", meaning a person qualified under 49 CFR 213.238.
Three points are often misread:
- 213.237 names no method. The word "ultrasonic" appears nowhere in Part 213. Ultrasonic testing is the industry's standard way to meet the rule, not a named requirement.
- Part 213 has no rail corrosion or thickness limit. A search of the 2025 Part 213 text on govinfo finds no use of "corrosion", and "thickness" appears only in the crosstie rules (tie plate cutting in 213.109 and 213.335).
- The intervals cover Class 3 to 5 track. On Class 4 and 5 track the limit is 370 days or 30 MGT, whichever comes first; see 49 CFR 213.237 rail flaw detection requirements for the full schedule.
Key takeaway: for a compliance test, the tool question is already answered: flaw detection equipment run by a 213.238 qualified operator.
Which rail jobs need a flaw detector?
Any job that asks whether a crack or internal defect is present needs a flaw detector: the scheduled internal rail search, hand verification of suspects, field weld inspection and bolt-hole checks. Frogs are the exception, because cast manganese steel defeats conventional UT.
Scheduled internal rail testing
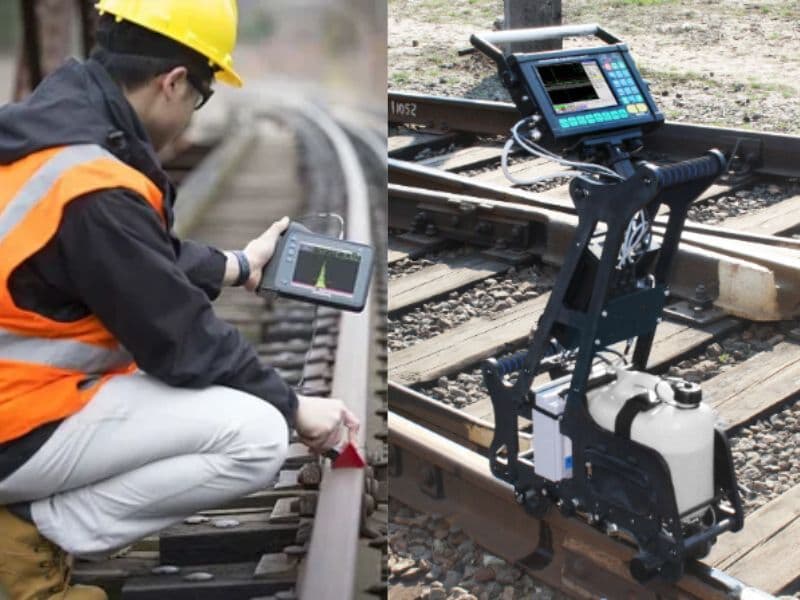
The 213.237 search finds transverse fissures, detail fractures, compound fissures, vertical and horizontal split heads, bolt-hole cracks and head-web separations. A test car, a hi-rail-mounted system or a walking cart is a multi-channel flaw detector on wheels: typically a 0° channel plus angle channels around 37–45° and 70°. The 70° beams cover transverse defects in the head, the 0° beam finds horizontal planes and loss of back wall, and the 37–45° beams reach the web and bolt holes. Our guide to the ultrasonic flaw detector for rail inspection explains the probe set in more detail.
Verifying suspects
Under continuous testing, the test must produce a listing of suspect locations "identified so that a person qualified under § 213.238 can accurately locate and field-verify each suspected defect" (49 CFR 213.240(e)). That field verification is hand testing with a portable flaw detector. The operator confirms the defect type and estimates its size, because the remedial action in 49 CFR 213.113 depends on both. A thickness gauge gives neither. For how the two testing modes differ, see continuous vs stop-and-verify rail testing.
Field welds
Thermite and flash-butt welds are inspected with a flaw detector and angle-beam probes, to the owner's weld specification (AREMA Manual for Railway Engineering Chapter 4 practice and, where adopted, AWS D15.2/D15.2M:2022). The rail base deserves particular attention. A TTCI survey of thermite weld failures (TD-00-013, July 2000) noted that "the ultrasonic rail flaw detection process only scans the head and web of the rail, and not the majority of the base". That is why field welds need hand UT of the base, which only a flaw detector can provide. Our page on aluminothermic weld inspection covers the weld side.
Frogs and other special trackwork
Most main-line frogs and crossing diamonds are cast austenitic manganese steel. FRA-sponsored research (RR 22-25, 2022) describes the material as "highly attenuative" and coarse-grained, and reports that revenue-service examinations of these components "currently use only visual inspections". A flaw detector still applies to the rolled-rail parts of a frog, its joints and the welds that join it to the running rail. The cast body is a visual and penetrant job (manganese steel is essentially non-magnetic, so MT doesn't work), with research methods such as low-frequency SAFT under development. See railroad switch and crossing inspection for the turnout side.
Key takeaway: cracks, welds and suspects are flaw-detector work; the cast body of a manganese frog is not reliably either tool's work today.
When is a thickness gauge the right tool on a railway?
A thickness gauge is the right tool when the question is section loss from corrosion: the rail web and base in tunnels and under crossings, steel bridge members, tanks and other steel structures. In each case the owner needs a number to compare with an original thickness or an engineering limit.
Rail web and base corrosion in tunnels and crossings
Corrosion of the rail foot and web concentrates where the rail stays wet and can't be seen. The EU-funded MONITORAIL project put it this way: "Defects in the foot are more likely where corrosion is more severe, such as at level crossings or in tunnels" (CORDIS project 262194). Tunnel seepage, condensation and blocked drains keep the foot wet, and slab track or embedded fastenings hide it.
The best-documented case is a 2019 Canadian derailment at a road crossing. The Transportation Safety Board of Canada found the rail web had corroded from 14.28 mm to about 4 mm under the crossing surface, and that rail flaw UT "is not currently designed to identify rail web and base corrosion at crossings" (TSB report R19M0018). The rail had passed an ultrasonic test about three months earlier. Our articles on tunnel rail inspection and grade crossing rail inspection cover both settings.
Where the web and base can be reached, a dual-element gauge on cleaned steel gives the remaining section; its crossed beams are more sensitive to pit bottoms than a single-element probe, and the readings can be trended between visits.
Steel bridge members
On steel railroad bridges, thickness gauging quantifies section loss in girders, floor beams, truss members and gusset plates. FHWA's bridge technology page states that "Thickness gages are commonly used for the detection of section loss resulting from corrosion in steel bridge members", and that the method suits components "with a plate-like geometry" (FHWA InfoTechnology). It also lists surface preparation and trained operators as requirements. The bridge itself falls under the owner's bridge safety program in 49 CFR Part 237, with inspection at least once each calendar year and no more than 540 days apart (237.101). Rail flaw testing on the deck and approaches stays under 213.237. See railway bridge inspection.
Tanks and other structures
Fuel and storage tanks at yards and shops, and steel structures such as platforms, canopies and pipe supports, are classic thickness-gauge work. Aboveground storage tanks are commonly inspected under API Standard 653 (fifth edition, 2014, with addenda through 2025; check the edition your inspector works to). Thickness readings feed a corrosion rate and a remaining-life estimate. Our guide to ultrasonic thickness measurement methods works through that calculation, so it isn't repeated here.
Key takeaway: a thickness gauge earns its place wherever metal is wasting away and the owner needs a trendable number, and on track that means mainly the web and base at wet, hidden locations.
How is rail head wear measured, if not with a thickness gauge?
Rail head wear is measured with rail wear gauges and calipers, gauge face angle gauges, and contact or laser profile systems, against the new-rail profile for that rail section, not with an ultrasonic thickness gauge. The original version of this article got this wrong.
Head wear has three parts: vertical head loss, side wear on the gauge face, and the gauge face angle. Each is defined against the design profile. A 0° ultrasonic reading taken on the head gives total rail height at one point, and nothing about side wear or the shape of the worn head. Wear limits are written as profile measurements, so they need profile tools.
| Tool | What it measures | Where it fits |
|---|---|---|
| Rail wear gauge or caliper | Side wear and head height loss at set points | Routine readings on curves and switches |
| Gauge face angle gauge | Whether the worn face is steeper or flatter than a set angle | High rails and switch points where wheel climb is a concern |
| Contact or laser profile system | The full head profile overlaid on the design profile | Grinding planning, wear rates, head area loss |
| Track geometry car with rail profile system | Repeated profiles over long distances | Network trending, with field verification of exceptions |
Part 213 sets no running-rail head or side wear limit. It limits gage (213.53) and wear on joint bars, switch points and frogs. Wear limits come from railroad standards and AREMA practice. NTSB has asked railroads to "use methods that accurately measure railhead wear" (Safety Recommendation R-08-11), partly because a worn head changes how ultrasonic rail testing performs. Our article on gauge face wear covers the measurements, the gage rule and the wheel-climb link.
Key takeaway: head wear is a profile question, so neither the thickness gauge nor the flaw detector is the right tool.
Thickness gauge vs flaw detector: which tool for which job?
The table below maps common railway inspection jobs to the right tool, the rule or standard behind the job, and the reason. Where a job needs both, it says so.
| Job | Tool | Rule or standard | Why |
|---|---|---|---|
| Scheduled internal rail test, Class 3–5 | Flaw detection system (test car, hi-rail system or walking cart) | 49 CFR 213.237, 213.238, 213.241 | Only a continuous search by a qualified operator counts as a valid search |
| Verifying suspects from a continuous test | Portable flaw detector, 0° and angle probes | 213.240(e), 213.113 | Type and size set the remedial action |
| Bolt holes and rail inside joint bars | Flaw detector, 37–45° and 0° | 213.237(f) | The rule requires detection between joint bars |
| Thermite or flash-butt field weld | Flaw detector, angle beams plus base scanning | Owner weld spec; AREMA MRE Ch. 4; AWS D15.2:2022 where adopted | Test cars miss most of the base |
| Cast manganese frog body | Visual and PT; UT only as research | FRA RR 22-25 | Coarse grain scatters conventional UT |
| Rail web and base corrosion (tunnels, crossings) | Dual-element thickness gauge plus visual | No Part 213 limit; owner engineering limit | Section loss needs a number; rail flaw UT isn't designed for it (TSB R19M0018) |
| Rail head wear | Wear gauge, angle gauge, laser or contact profile | Owner standards, AREMA practice; NTSB R-08-11 | Wear is defined against a profile |
| Steel bridge member section loss | Thickness gauge after surface preparation | 49 CFR Part 237 bridge program | Plate-like members give clean back-wall echoes |
| Cracks at bridge welds and details | Flaw detector, angle beam | Bridge owner's program; contract code | Fatigue cracks are planar and need angle beams |
| Structural steel welds (buildings, platforms) | Flaw detector, angle beam | AWS D1.1, when the contract calls for UT | D1.1 rates indications from an angle-beam A-scan |
| Storage tank shell and floor | Thickness gauge, scanning where the inspector requires it | API 653 | Corrosion rate and remaining life |
Key takeaway: if the job's standard asks for an indication rating or a valid search, it's a flaw detector; if it asks for a minimum thickness or a corrosion rate, it's a gauge.
Worked example: a tunnel job that needs both tools
A typical tunnel job needs the flaw detector for the 213.237 search and a thickness gauge for the wet low points, and the possession window has to fit both. The inputs below are stated assumptions for illustration, not a quote or a standard production rate.
The job
A transit agency has a 0.8-mile tunnel section of 136RE rail on track subject to 213.237. Its last visual inspections flagged three wet low points with visible foot corrosion, each about 120 ft long. The agency wants a valid internal search of both rails, verification of any suspects, and a thickness survey of the web and base at the three low points, all in one 4-hour night possession.
Step 1: the time available
Assume 30 minutes for protection set-up and power-down verification at the start, and 30 minutes to clear at the end.
- Working time = 240 − 30 − 30 = 180 minutes
Step 2: the flaw detection search
Assume a two-rail walking cart at an average 1.0 mph, including stops.
- Search time = 0.8 mile ÷ 1.0 mph = 0.8 h = 48 minutes
- Allowance for hand verification of two suspects at 15 minutes each = 30 minutes
- Flaw detection total = 48 + 30 = 78 minutes
If a suspect sits at a bolted joint, the operator verifies the bolt hole with a 37° probe. On 136RE the bolt-hole center is 4.22 in. below the running surface (7.3125 in. rail height less 3.0938 in. hole height above the base). The sound path to the hole center is 4.22 ÷ cos 37° = 5.28 in., and the probe sits 5.28 × sin 37° = 3.18 in. from the hole along the rail. The depth (4.22 in.) is less than the rail height (7.31 in.), so the geometry is possible.
Step 3: the thickness survey
The survey grid takes a reading every 5 ft at three points per rail: mid-height of the web, and the top of the base flange on the field and gauge sides.
- Stations per zone = 120 ÷ 5 + 1 = 25
- Readings per zone = 25 stations × 2 rails × 3 points = 150
- Readings for three zones = 150 × 3 = 450
- At an assumed 30 seconds per reading, including scraping scale to bare steel: 450 × 30 = 13,500 s = 225 minutes
One technician can't finish 225 minutes of survey in a 180-minute window. Two thickness technicians working in parallel need 225 ÷ 2 = 112.5 minutes each. That fits beside the 78-minute flaw crew with about 67 minutes to spare, if the survey crews and the cart work different zones.
Step 4: reading the numbers
The gauge is calibrated on a steel block at an assumed longitudinal velocity of 0.2320 in./µs (calibrate on the actual material; velocities differ between steels).
Web. The 136RE web is nominally 11/16 in. (0.6875 in.).
- Expected round trip = 2 × 0.6875 ÷ 0.2320 = 5.93 µs
- Worst reading in zone 2: round trip 4.48 µs, so thickness = 0.2320 × 4.48 ÷ 2 = 0.520 in.
- Loss = 0.6875 − 0.520 = 0.1675 in., or 0.1675 ÷ 0.6875 = 24.4%
Base flange. The base flange tapers, so there's no single nominal value at the reading point. The crew takes a baseline at the same offset on dry, uncorroded rail at the tunnel portal: 0.620 in.
- Worst base reading in zone 2: 0.410 in.
- Loss = 0.620 − 0.410 = 0.210 in., or 0.210 ÷ 0.620 = 33.9%
Step 5: what the agency does with it
Neither result is a Part 213 defect, because Part 213 has no corrosion limit. The agency's engineer compares the losses with the agency's own limit and decides on monitoring or replacement. The flaw report goes in the 213.241 records; the thickness survey becomes the next visit's baseline.
Key takeaway: in a wet tunnel, the flaw search proves compliance and the thickness survey shows where the rail is wasting. One without the other leaves a gap.
Can one instrument do both jobs?
Yes, within limits: most digital flaw detectors have a thickness readout, many thickness gauges show a live A-scan, and some flaw detectors offer a corrosion module. A combined instrument suits mixed hand-testing jobs, such as verifying a suspect and then measuring web loss at the same joint.
The trade-offs are real, though:
- V-path correction. Dual-element probes read slightly high on thin sections because the sound path is a V, not a straight line. Thickness gauges correct this with probe-specific tables. A 2012 patent filing by Olympus NDT (US 8,156,784) states that flaw detectors generally don't.
- Precision. Evident's guidance says flaw detectors can measure thickness reasonably well but aren't designed for precision thickness work.
- Sizing. A thickness gauge has no DAC, TVG or DGS tools and no angle-beam set-up, so it can't rate a weld indication or verify a rail defect.
- The rail search itself. A handheld unit of either type isn't a 213.237 search system for miles of track. That search needs a multi-channel system with continuous coverage and a 213.238 operator.
If the procedure calls for angle-beam set-up and indication evaluation, the instrument must be a flaw detector. See digital vs analog flaw detectors for instrument features.
Key takeaway: a combined instrument saves carrying two boxes, but the procedure, not the brochure, decides which mode the job needs.
What can't either tool do?
A thickness gauge can't find cracks, and a flaw detector set up for a rail search isn't designed to measure section loss; neither one measures head wear, and neither sees through every surface condition. These limits should be written into the scope of any inspection.
- Thickness gauges miss planar flaws. A crack lying parallel to the beam, or one that doesn't block the back wall, leaves the thickness reading unchanged.
- Thickness gauges need parallel surfaces. ASTM E797 is "primarily for flat components with parallel surfaces". The rail head and the fillet areas of the web and base don't qualify, so readings belong at mid-web and on the flat of the flange.
- A single reading misses isolated pits. Spot readings sample a point. Pitting needs a dense grid or a scanned survey.
- Rail flaw UT doesn't cover all of the base. Vehicle and cart searches cover the head and web and the base under the web. The base flanges, where tunnel corrosion often starts, are largely outside the search.
- Surface condition limits both tools. Shelling, head checks and heavy scale block or scatter the beam. Lost coupling over a length of rail makes that length untested under 213.237(g), not passed.
- Coatings mislead plain pulse-echo readings. Paint is read at steel velocity, so the reading is high. Use an echo-to-echo mode or remove the coating.
Key takeaway: state in the scope what each tool covers, so a clean flaw report isn't read as proof that the rail foot is sound.
How EMA Industries applies this
EMA Industries provides ultrasonic rail flaw testing for transit agencies, short lines and industrial track owners, along with rail weld inspection, AWS D1.1 structural weld UT, MT and PT, and NDT Level III services. Based in Southern California and mobilizing nationwide, EMA Industries brings flaw detection to the 213.237 search, suspect verification and rail welds, and its Level III services can help write a scope that also states where corrosion needs thickness readings. To plan testing for a tunnel, crossing or bridge, contact EMA Industries.
Frequently asked questions
Can a thickness gauge be used for FRA rail testing?
A thickness gauge can't satisfy 49 CFR 213.237. The rule requires internal rail inspections that detect defects, including between joint bars, run as a valid search by a 213.238 qualified operator. A gauge reports one back-wall distance at one point and can't find a transverse fissure or a bolt-hole crack.
Can a flaw detector measure thickness?
Most digital flaw detectors have a thickness readout from the 0° echo, and some have a corrosion module. They work well for occasional readings. For large corrosion surveys with dual probes, a dedicated thickness gauge is usually better, because it corrects the V-path error and is built for pitting and thin-wall readings.
How do you check rail web and base corrosion?
Start with a visual inspection in good light, then clean the steel and take thickness readings with a dual-element probe at mid-web and on the flat of the base flange. Compare them with a baseline from dry rail of the same section. Focus on tunnels, crossings and wet low points, where rail flaw UT isn't designed to find section loss.
Is rail head wear measured with ultrasound?
Rail head wear is measured with wear gauges, calipers, gauge face angle gauges and contact or laser profile systems, against the new-rail profile. A 0° ultrasonic reading gives rail height at a single point only and tells you nothing about side wear or the shape of the head.
Sources
- 49 CFR 213.237, Inspection of rail, eCFR (text read on Cornell LII, October 2026)
- 49 CFR 213.238, Qualified operator, eCFR
- 49 CFR 213.240, Continuous rail testing, eCFR
- 49 CFR 213.113, Defective rails, eCFR
- 49 CFR Part 213, 2025 annual edition, govinfo XML (full-text search for "corrosion", "thickness" and "ultrasonic")
- 49 CFR Part 237, Bridge Safety Standards, eCFR
- ASTM International, E797/E797M-21, Standard Practice for Measuring Thickness by Manual Ultrasonic Pulse-Echo Contact Method
- Transportation Safety Board of Canada, Rail Transportation Safety Investigation Report R19M0018, released September 30, 2020
- European Commission CORDIS, MONITORAIL final report summary, project 262194
- FHWA, Bridge: Ultrasonic Testing (Thickness Measurement), InfoTechnology
- FRA Research Report RR 22-25 (ultrasonic inspection of cast manganese special trackwork; Wilson and Poudel), 2022, ROSA P
- TTCI, J. Kristan, Thermite Weld Failure Survey, Technology Digest TD-00-013, July 2000, PDF
- NTSB, Railroad Accident Report RAR-08/02 (New Brighton, PA), with Safety Recommendation R-08-11
- Evident, B. Kenaston, Thickness Gauge or Flaw Detector: Which Is Best for Your Application?, December 17, 2020 (vendor)
- Olympus NDT, US Patent 8,156,784, 2012 (V-path correction)